8D Report in Practice (Part 2): Permanent Solutions, Prevention, and Satisfying Auditors
In the first part, we successfully managed the initial chaos, implemented containment actions (D3), and most importantly, in step D4, we discovered two crucial things: Why the defect occurred (Development CAD data did not account for actual material shrinkage) and why it escaped to the customer (visual inspection is blind to this type of defect and technical detection was missing). Now we must fix the process permanently.
D5 and D6: Selection and Implementation of Permanent Corrective Actions (PCA)
Here you must eliminate the root cause itself. In the automotive industry, corrective actions must always be strictly divided into two independent branches: Action for the Root Cause of Occurrence and Action for the Root Cause of Non-Detection. Your PCA must cover both paths.
Let's show this on a real-world production example: The customer claims that interior parts assembled with a metal clip are not snapping together. You found that the operator physically mounted the clip onto the part's pin and snapped the parts together, but the hole in the plastic mating part was too large. After insertion, the clip lacked sufficient pre-tension (the locking tabs did not brace against the material edge), and popped out of the part during the slightest handling.
- Practical Tip (Action for Occurrence): Why was the hole too large? You uncovered an error in the part's design itself. The hole dimension in the CAD data was designed incorrectly regarding the actual material shrinkage. The corrective action for occurrence cannot be "instruct the operator to push the clip in better." The real action is an engineering change (ECR/ECO process). Drawings are updated, and the tool shop subsequently installs a new, narrower molding core (pin) into the injection mold. This allows more plastic to flow into that area, shrinking the hole in the part to the correct dimension, and the clip firmly locks upon insertion. Based on physics, the defect simply can no longer occur.
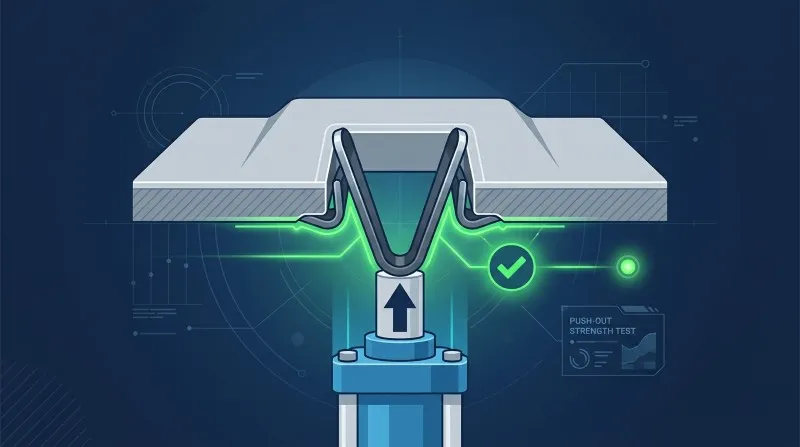
- Practical Tip (Action for Non-Detection): Why did the part with a loose clip escape the line? The operator pushed the clip in, it looked seated from the visible side, but it popped out during the transport of the packaging unit to the customer. Visual inspection is blind here. The action for non-detection is implementing a 100% mechanical anchorage test (a Push/Pull test) on the line. A pneumatic cylinder with a defined force (e.g., 20 N) is added to the End of Line (EOL) inspection fixture. The cylinder pushes against the clip in the opposite direction. If the hole is still too large, it won't hold the clip, and the cylinder will push it back. The cylinder's position sensor will register the extended stroke, trigger a NOK signal, and the system will block the printing of the OK label. The defective part is technically locked out.
- Show the data in D6: Now you must prove with hard data that the solution works (Verification of Effectiveness). Example for the report: "Engineering change approved, narrower core installed in mold No. 2, and pneumatic push-test installed at EOL. The verification run of 500 pcs proved clip pull-out forces are within tolerance. Since the modification, the line has produced 15,000 parts, and the escape of non-conformities to the customer (0 km claims) is zero."
D7: Preventive and Systemic Actions (Change the Company DNA)
Attention, this is where the absolute most common methodological mistake is made. Many people write in D7 that they modified a mold or added a sensor. No! Physical modifications to the process and line belong strictly in D5 and D6. No hardware modifications belong in D7; this is exclusively at the system level.
- Practical Tip: Here you must ensure that the experience gained from this error is transferred to the entire quality management system. You must update the FMEA (e.g., increase the Occurrence rating if it turned out that the visual check of the snap-fit is ineffective). This logically leads to the need to update or revise the Control Plan and the maintenance plan.
- Don't forget the Read-across (Lessons Learned): D7 also means taking a look around the rest of the shop floor. Do we happen to have a similar type of clip on a line for another customer? Is there a risk of the same error in a sister project? Apply prevention across the entire company. The customer wants to see that you learn from your mistakes across the board.
D8: Team Recognition and Closure
The customer has approved your actions, the claim is closed on the portal, and the scrap rate is zero. One last step remains.
- Practical Tip: Don't treat this point just as a formal checkmark in a spreadsheet. 8D reports are handled under immense pressure, escalations mean stress, and often overtime at the machine. Go out to the production floor and personally thank the toolmakers, operators, and process engineers who helped you save the situation. A quality engineer who cannot stand behind their team and thank people directly on the shop floor is lost in the long run; this is how you build the team's respect.